
The Pilbara presented a relentless construction environment: mini-tornado whirlwinds, oppressive heat, strong winds, cyclone alerts, and high-UV exposure throughout the program. Iron ore dust, nicknamed the "Pilbara Fog", blanketed the zone continuously, intensified by ore stockpiled on an adjacent hill. All while the site remained operational. Stringent safety protocols required multiple inductions and competency verifications before any works could begin.
The solution had to be fully sealed against both evaporation and dust ingress, leave minimal civil footprint, support nearby residents during water shortages, and deliver fill and drain flow rates of 250 L/sec without compromising liner integrity.
Solution
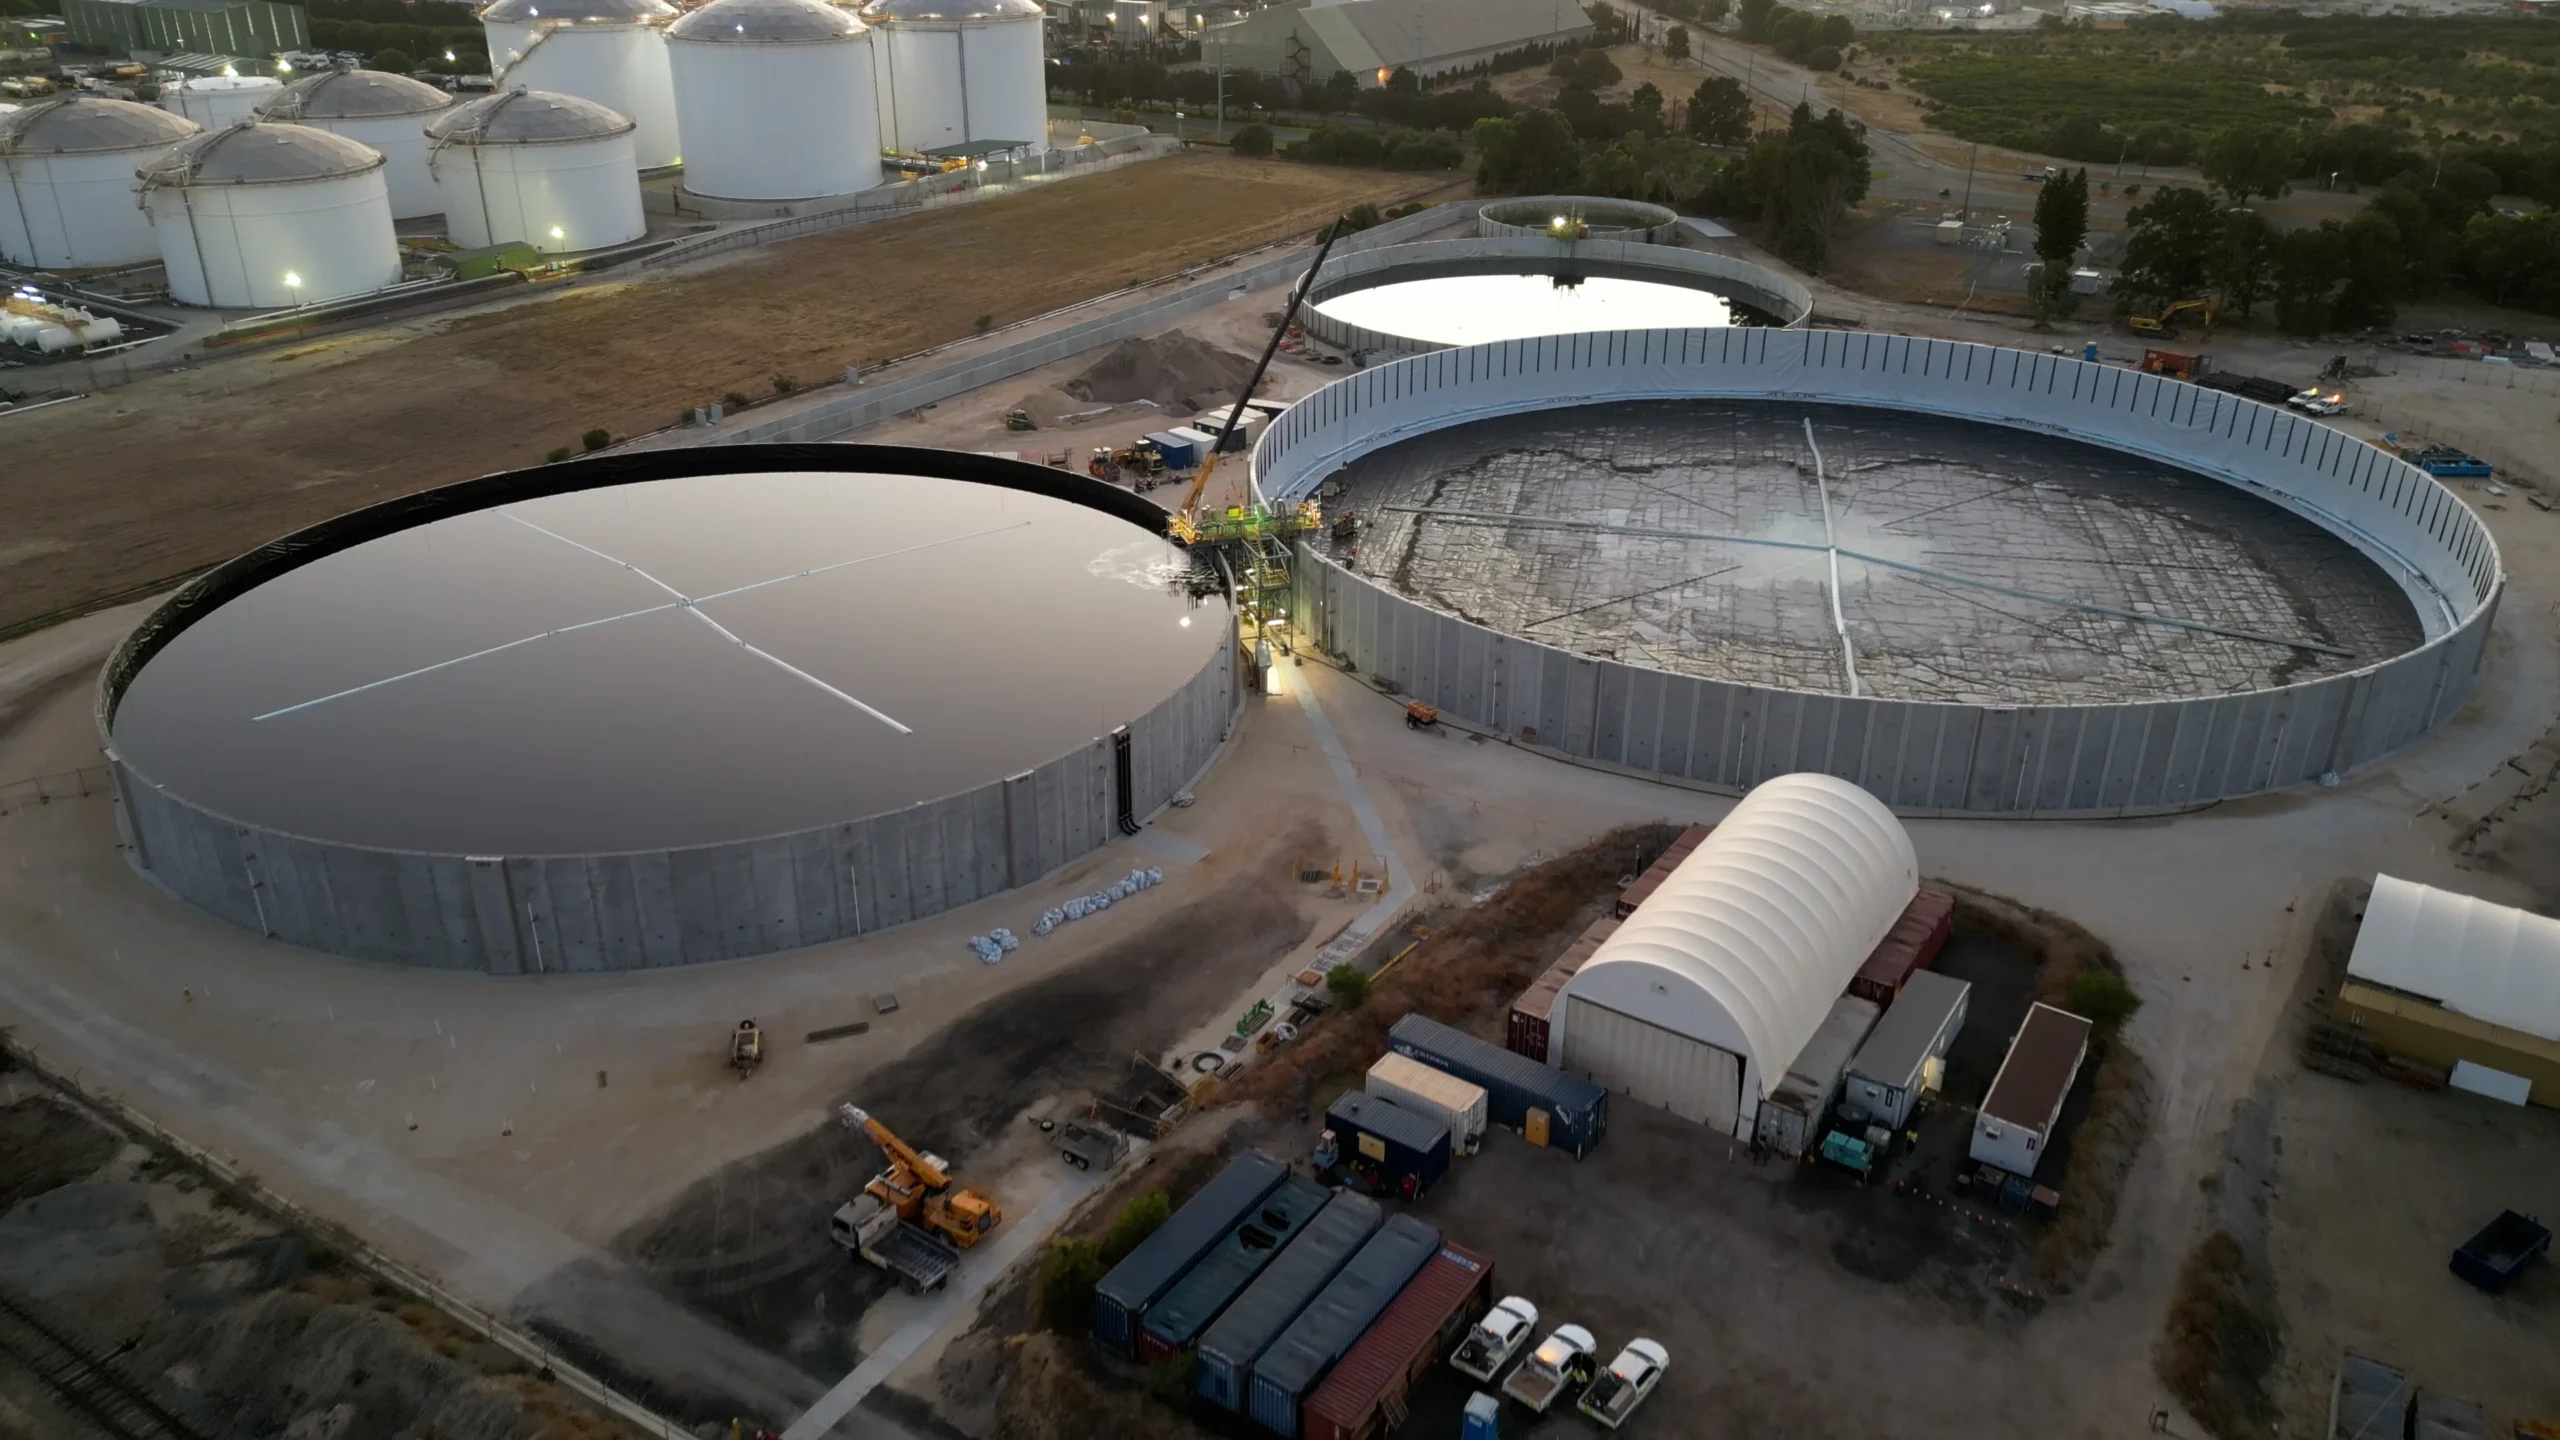
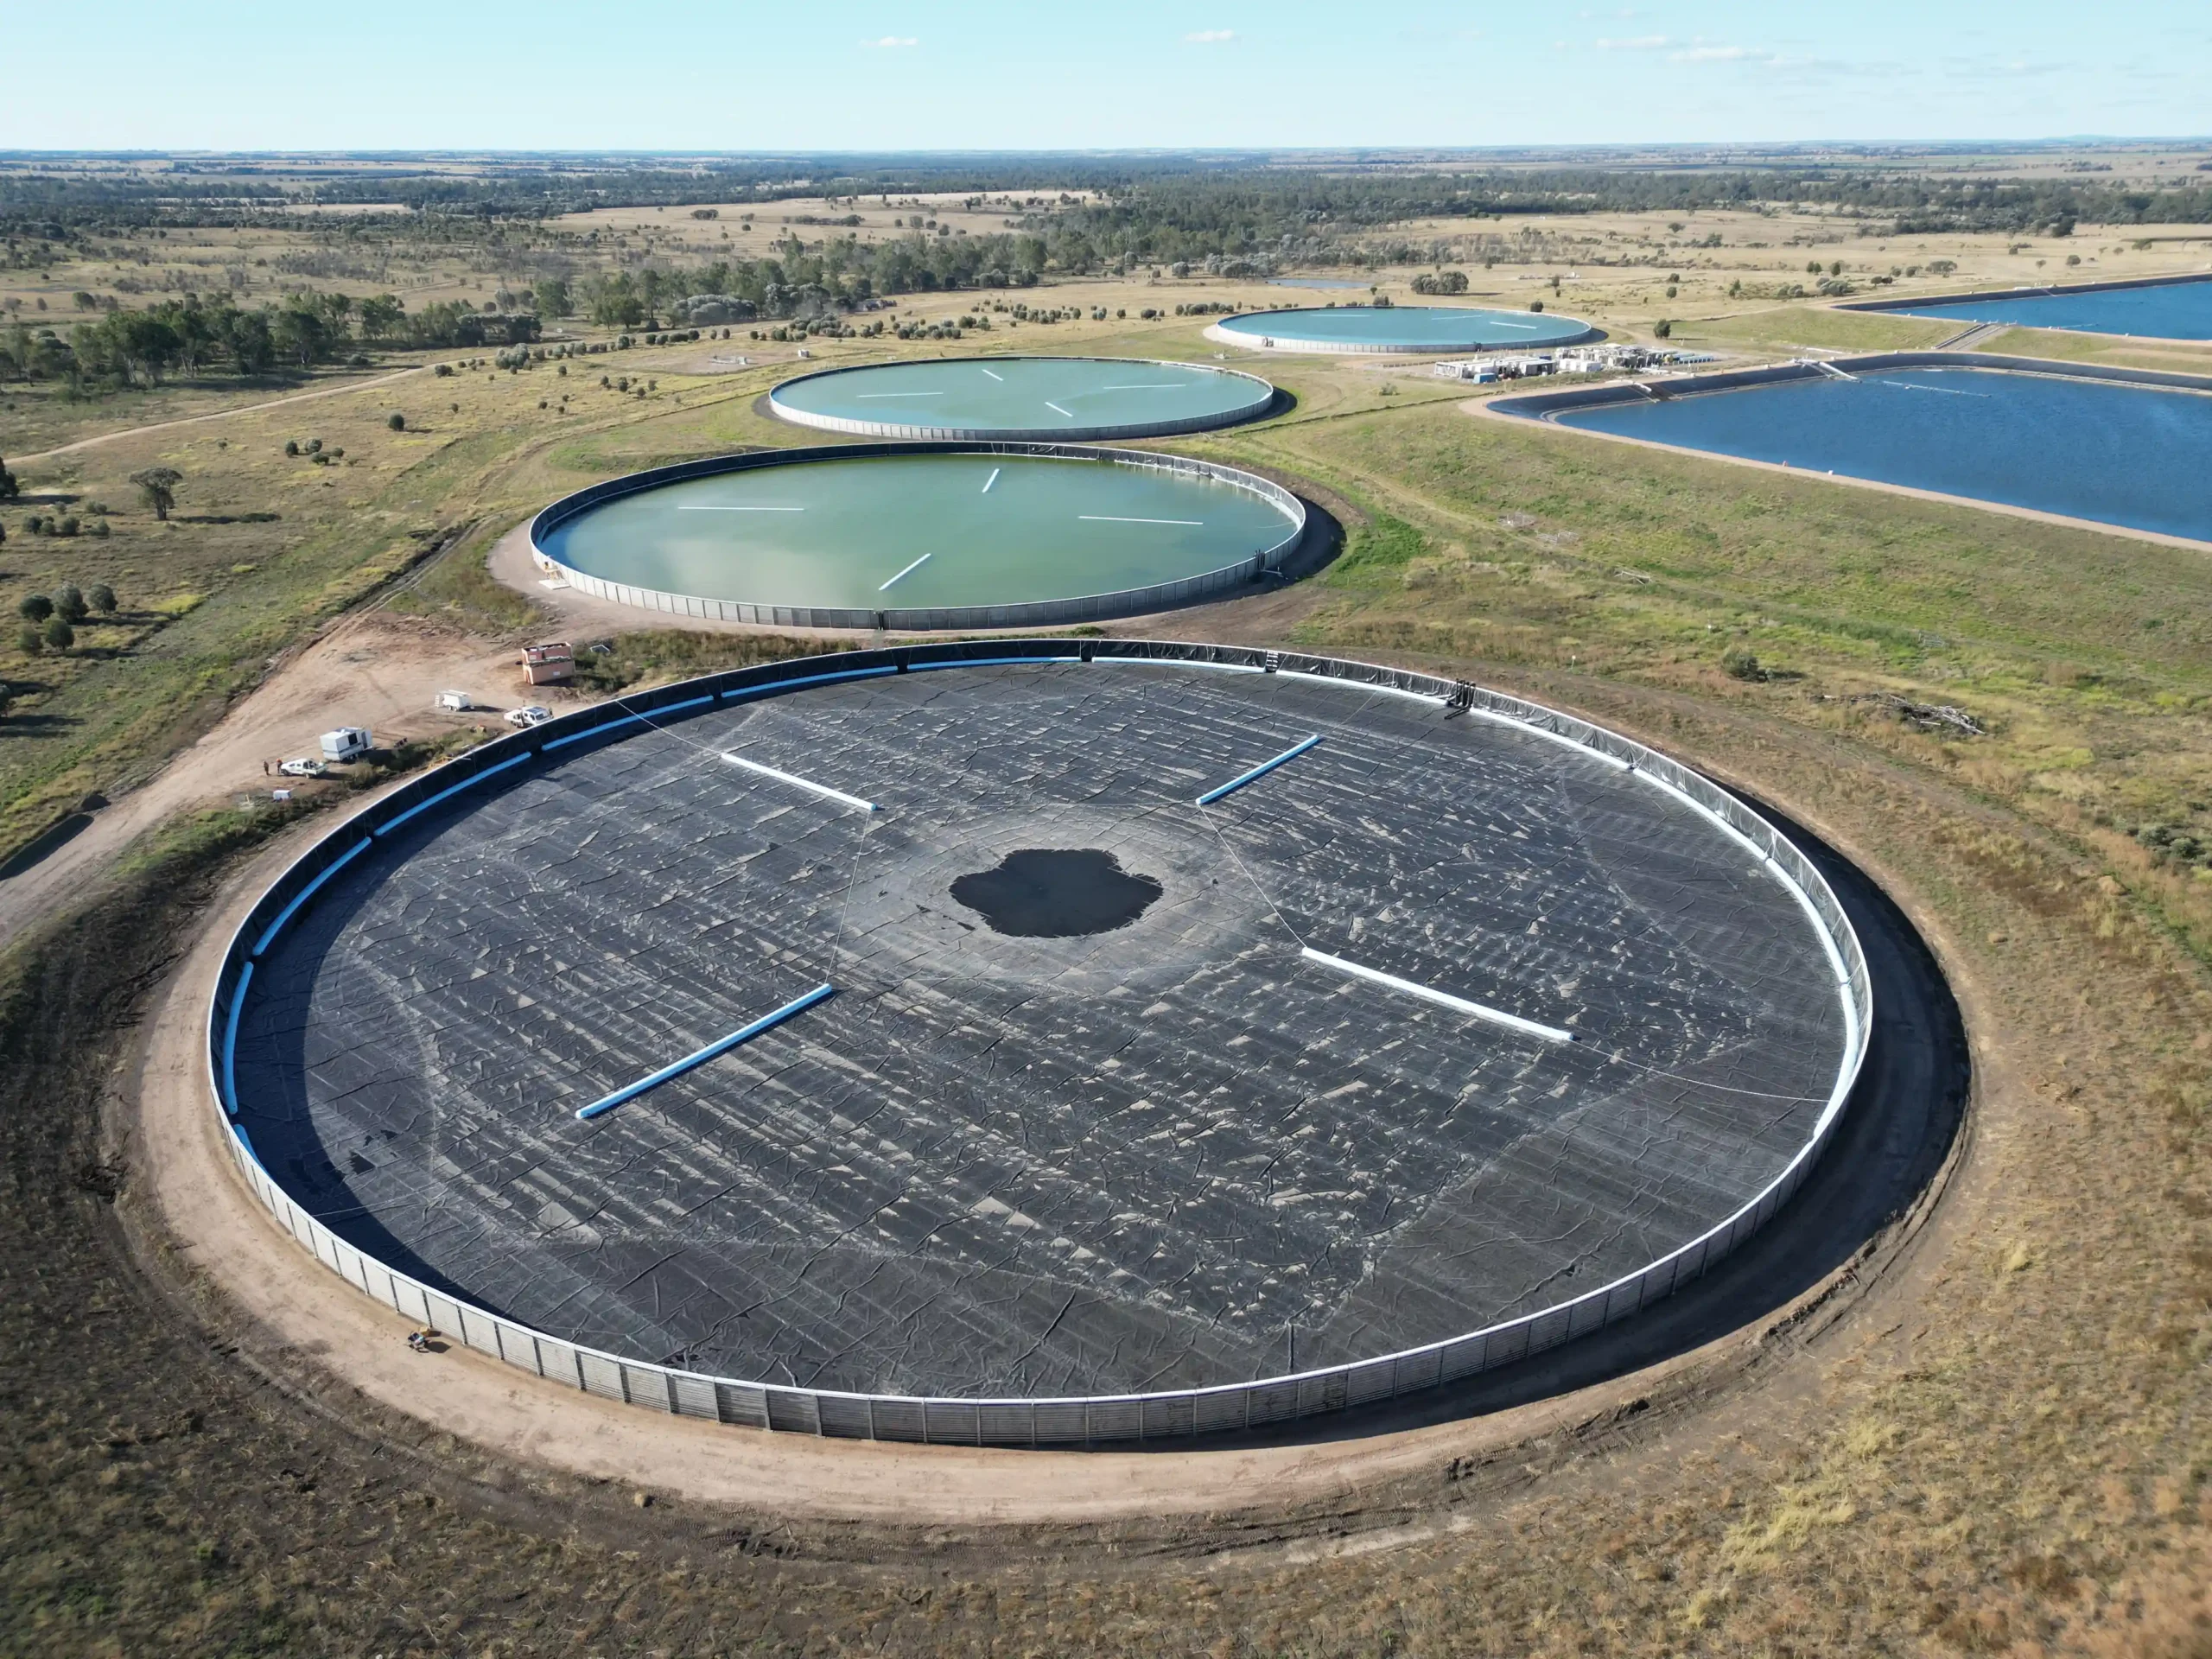
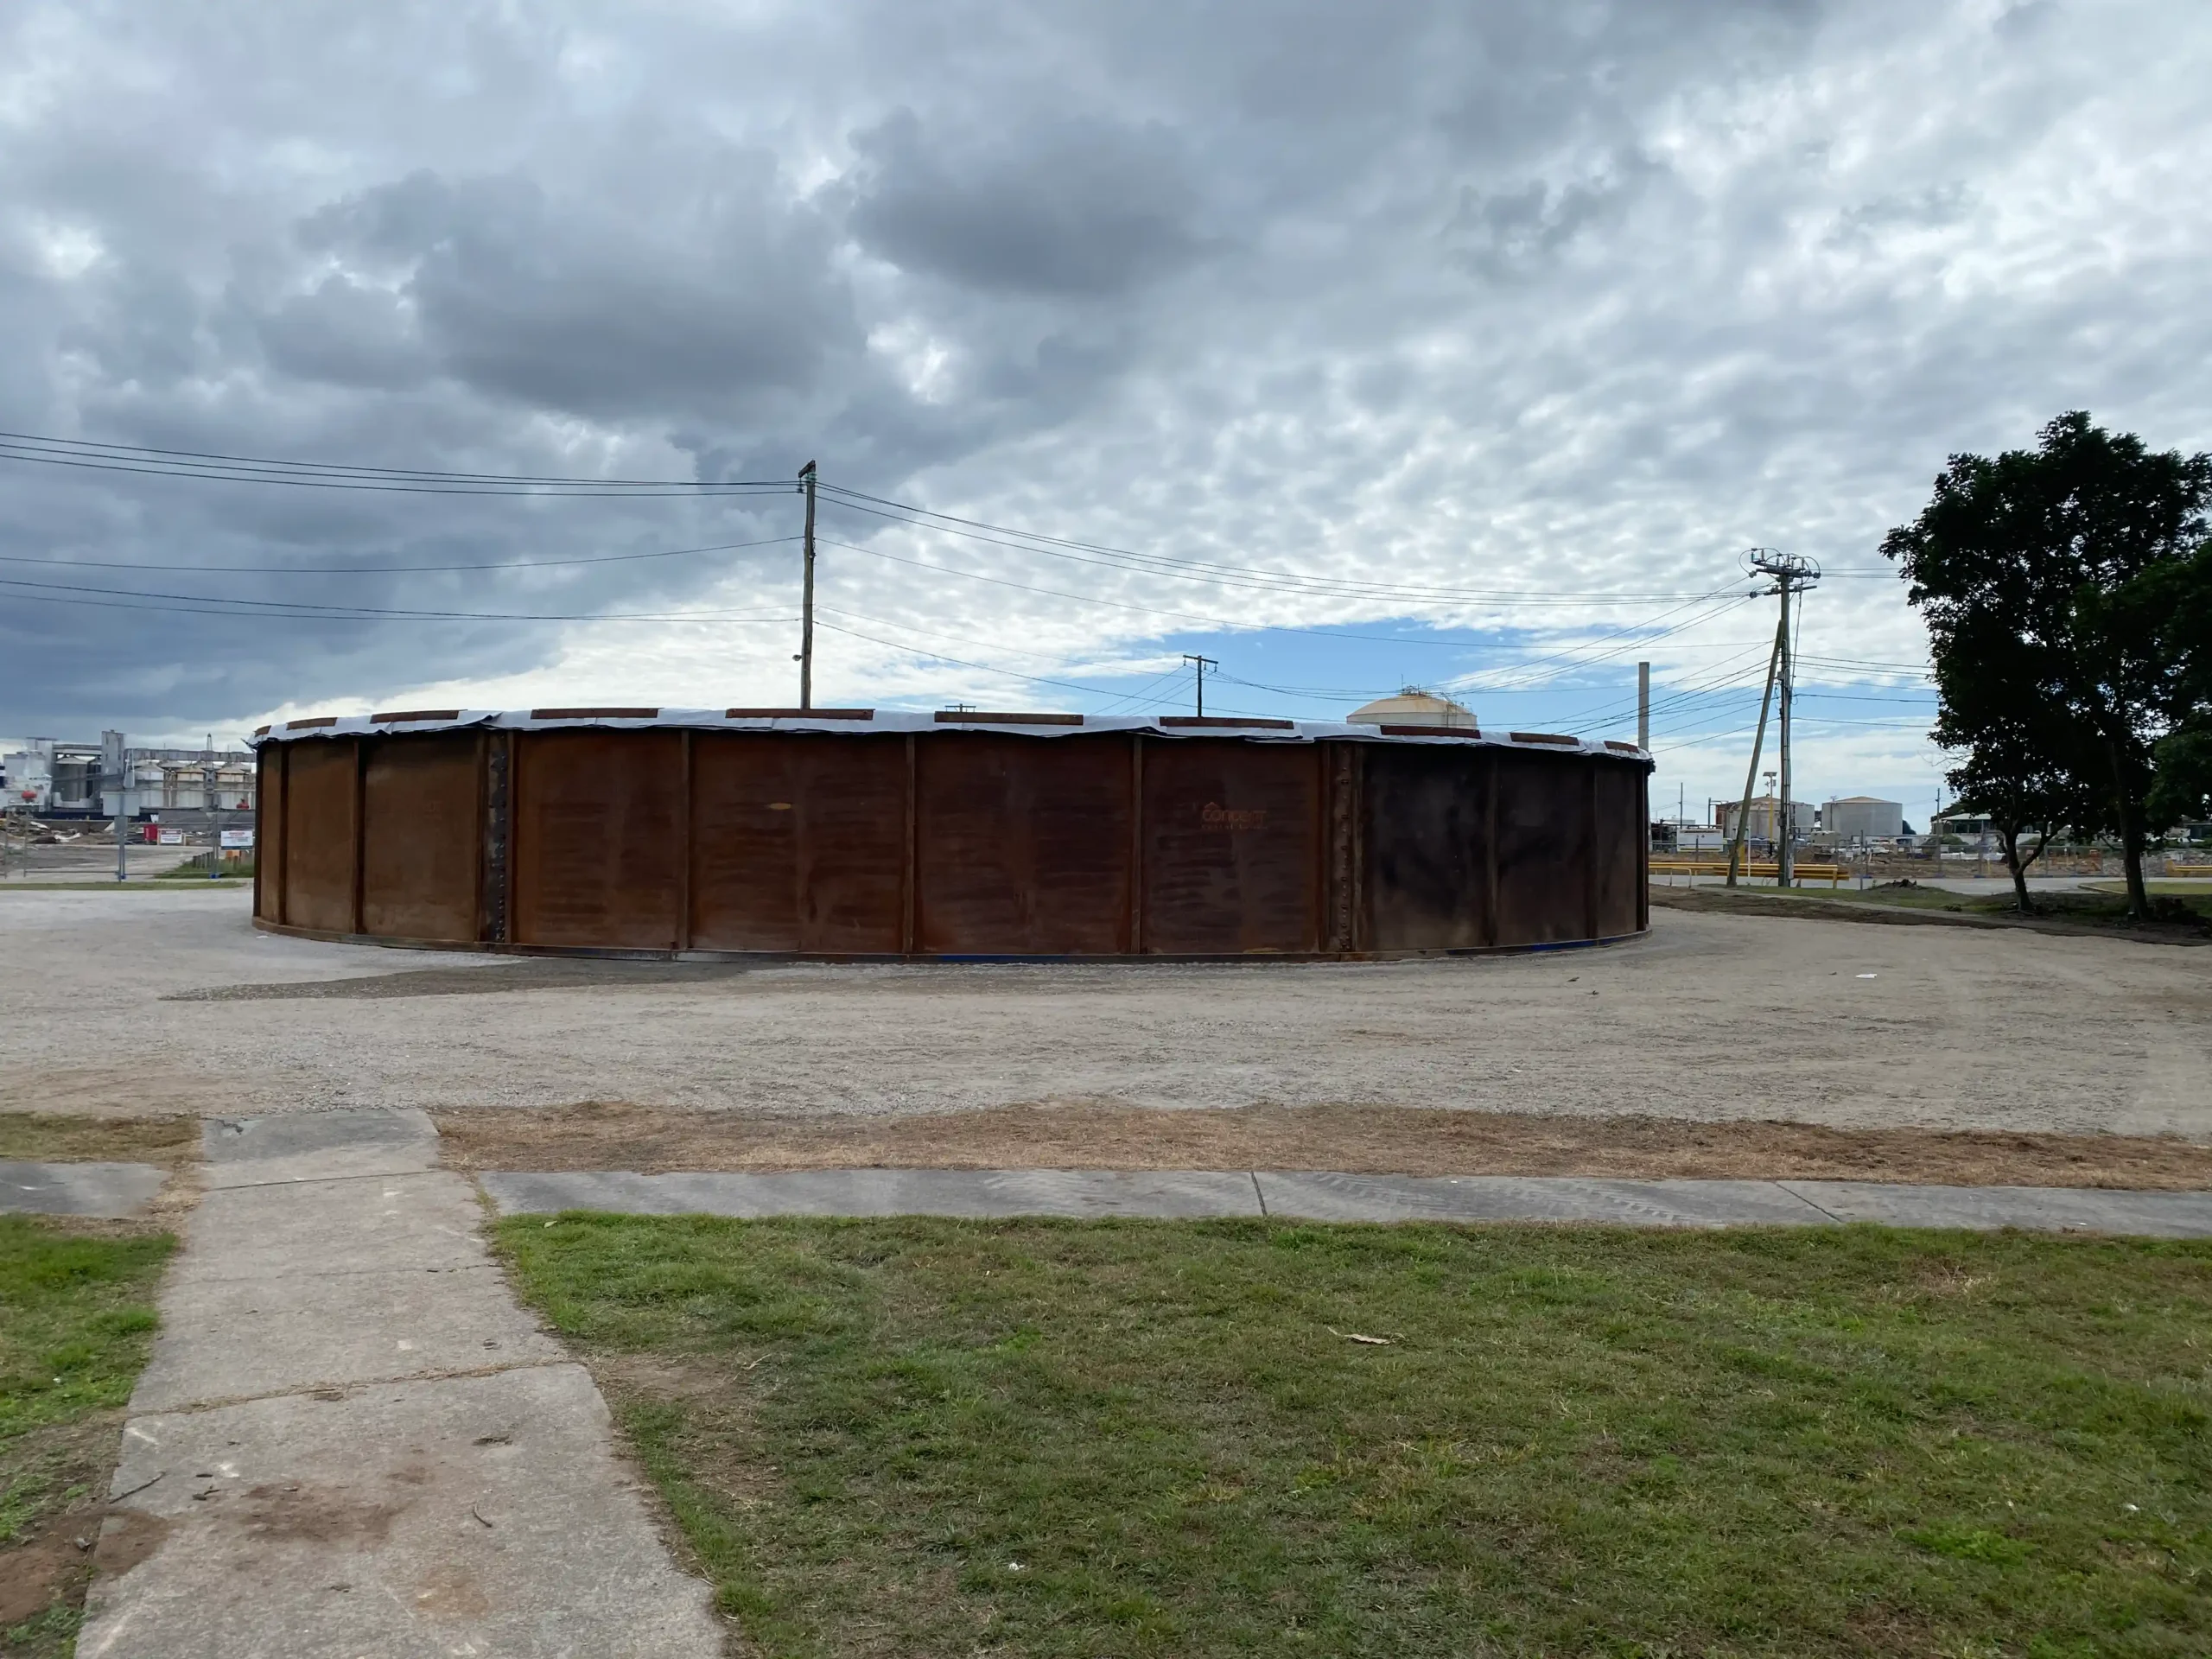
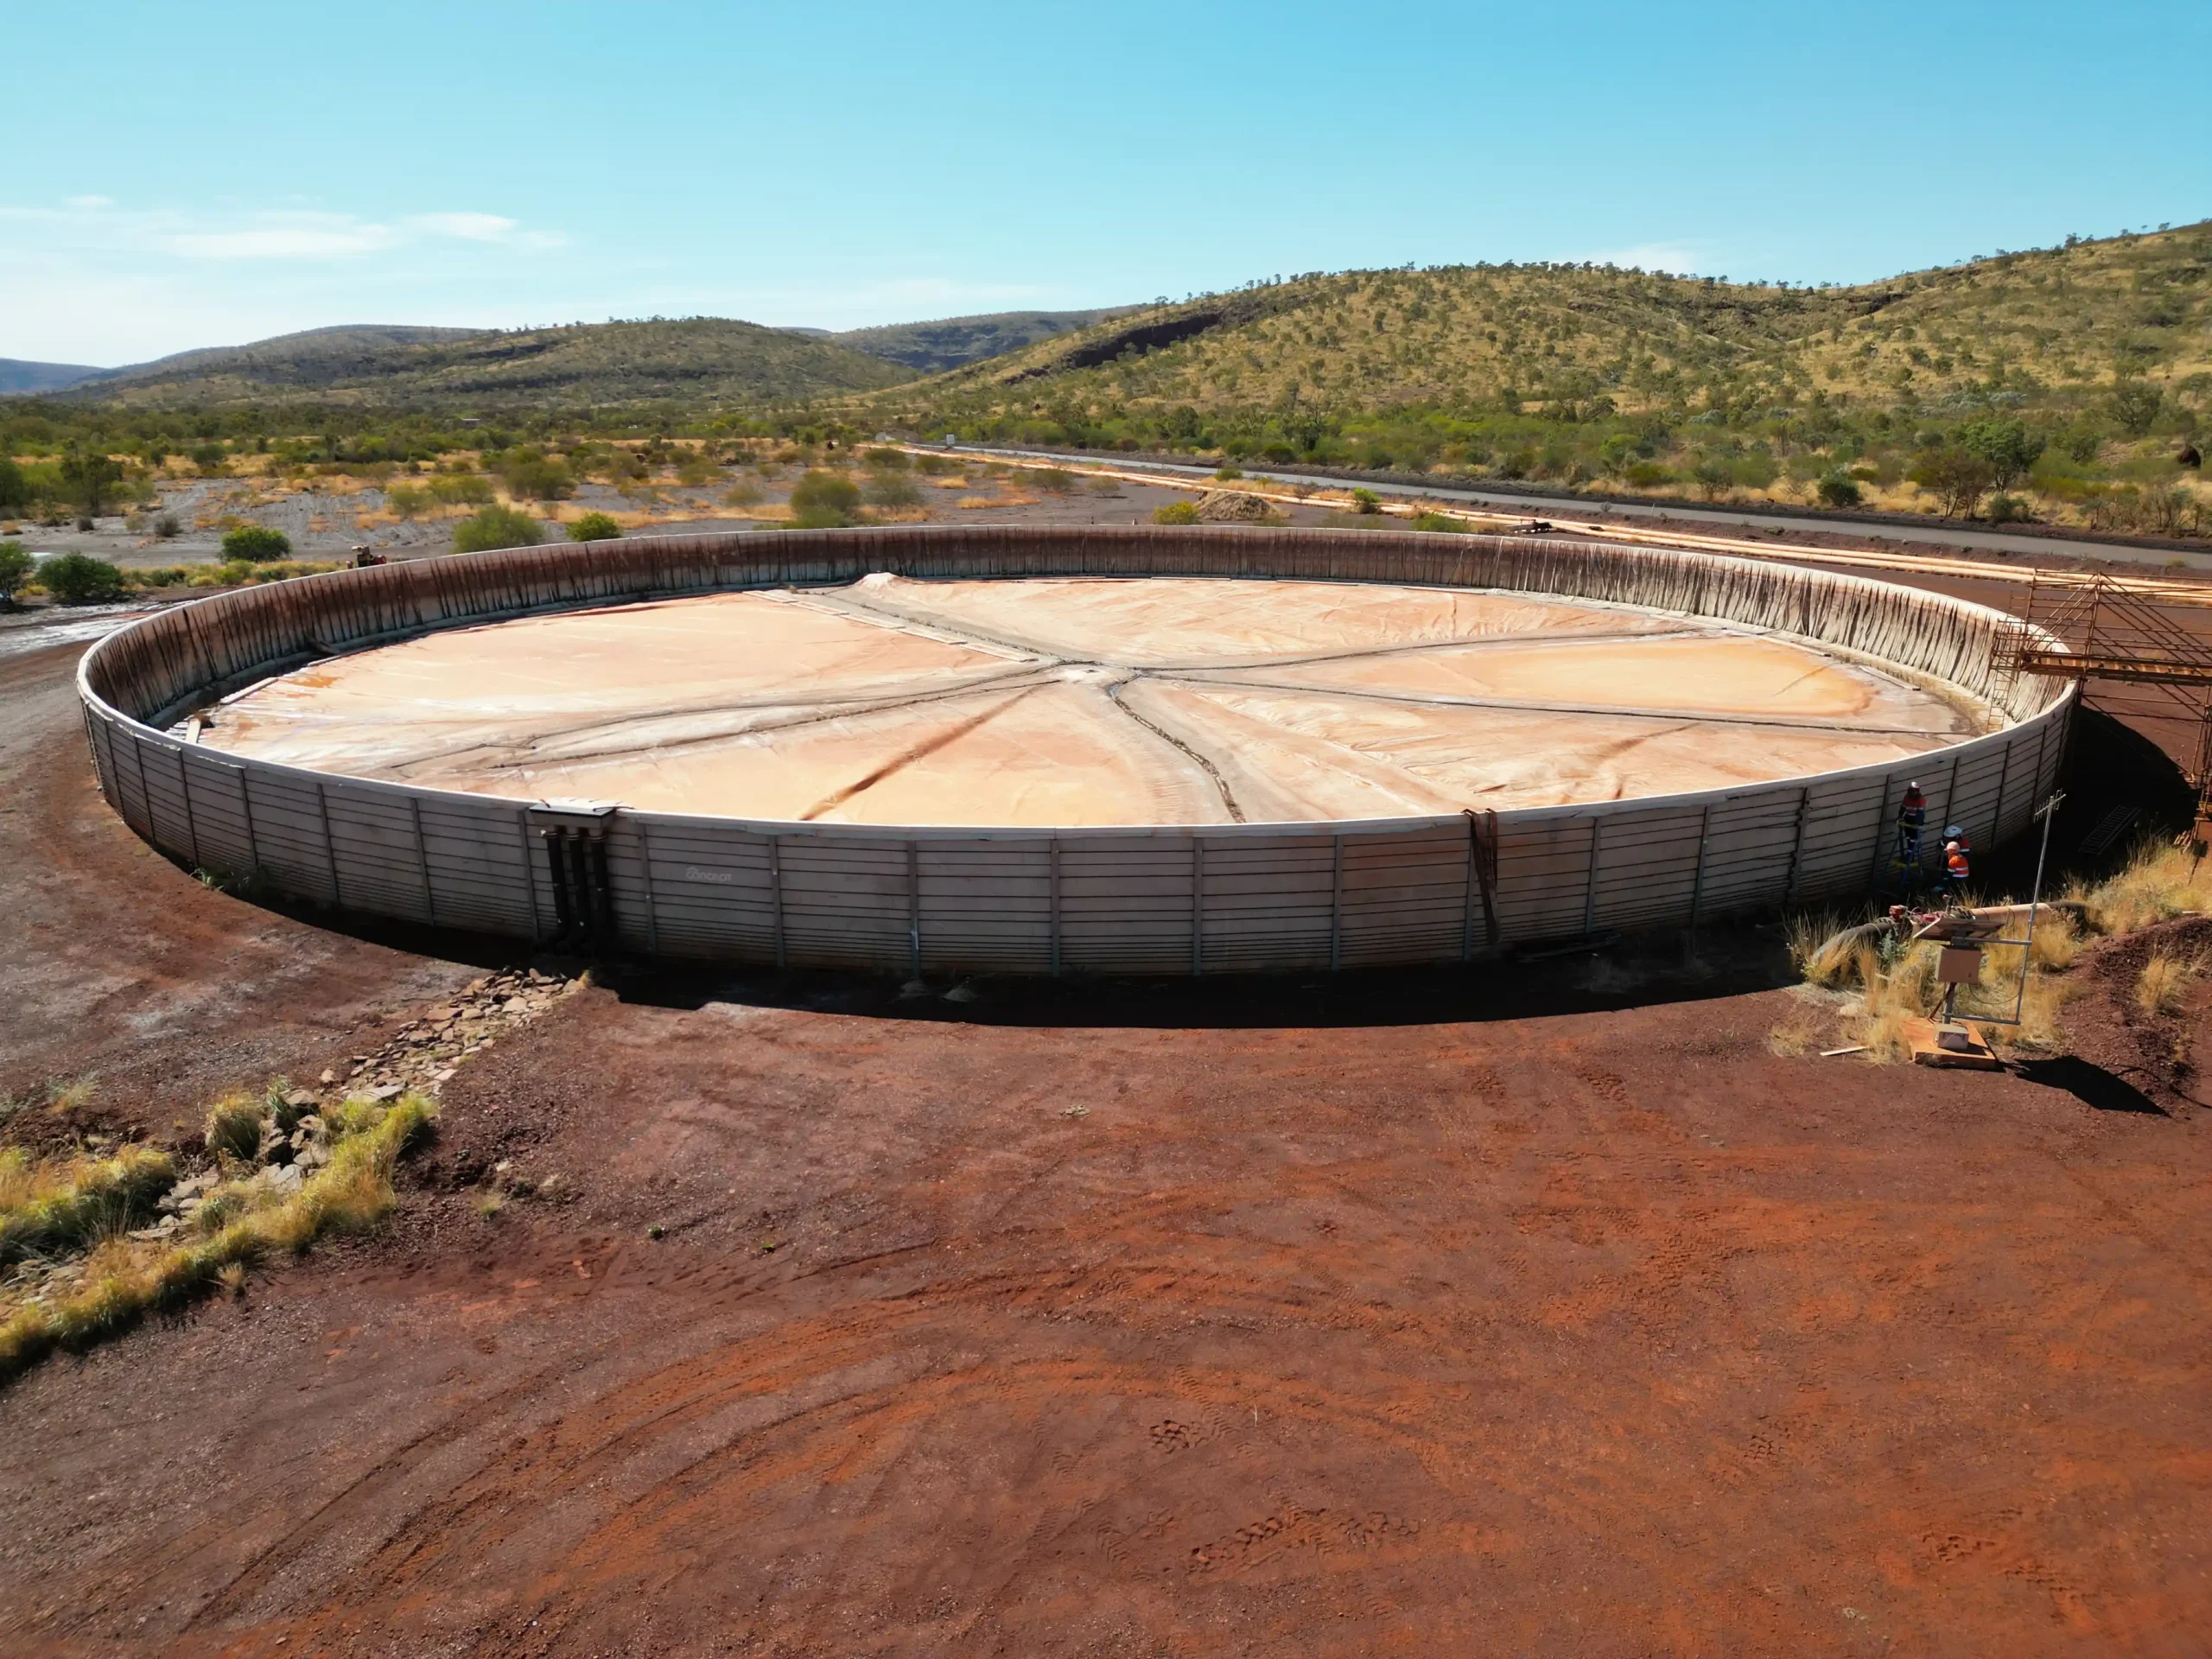
Concept Tanks supplied a 10 ML potable water Concept Tank™ with a 3.0 m wall profile and an Engineered Floating Cover; fitted with floats, vents, hatches, walkways, and a cover pump system, to combat evaporation and prevent dust and stormwater ingress. Pipework was routed through the tank floor for floating cover compatibility, and stainless-steel diffusers and vortex breakers were engineered into the penetrations to protect the liner at 250 L/sec flow rates. Where sand would typically correct rough subgrade patches, the crew sieved on-site Pilbara dust to remove ore particles and repurposed it directly.
Outcome
The Engineered Floating Cover delivered proven evaporation control and year-round water quality protection, while meaningfully reducing the customer's ongoing water treatment costs. The customer specifically praised the Engineered Floating Cover’s performance and subsequently engaged Concept Tanks to install two 1.4 ML Concept AST™ (Above-ground Storage Tanks) at a separate site.